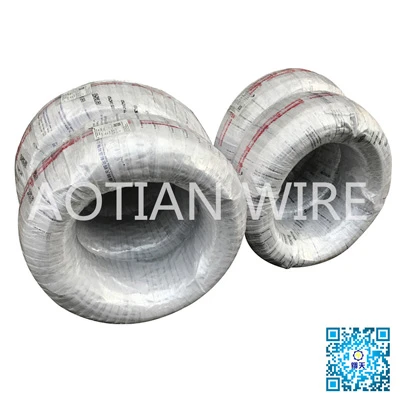


During cold heading forming of bolts, nuts and rivets, wire
scuffing is a common industrial pain point. Scuffing refers to strip‑shaped scratches and metal peeling on wire surface generated in wire‑drawing or cold heading extrusion, exposing base metal. Such defects will transfer to finished fasteners and undermine mass‑production stability.Scuffing originates from multiple links including raw material, heat treatment, phosphating‑saponification, drawing equipment and site operation.

First, failure of surface lubrication protection. Phosphating‑saponification is the key surface treatment for cold heading wire. Coarse phosphating crystals, improper coating weight, poor film adhesion, or insufficient drying of saponification layer will break the lubricating isolation layer under high‑pressure friction and trigger scuffing. Residual acid and sediment from insufficient water washing will also scratch wire substrate.
Second, abnormal substrate microstructure. Improper spheroidizing annealing leads to surface decarburization, causing uneven surface hardness. Irregular metal flow under deformation will result in repeated scuffing even with qualified phosphating‑saponification parameters, and accelerate die wear meanwhile. Residual scale and inclusions from raw wire rod are potential risk sources as well.Third, equipment and operational factors. Worn drawing dies, accumulated iron debris inside powder box, damaged guide rollers will scratch wire directly. Unstable drawing tension and disorder winding also contribute to continuous scuffing failures.
Scuffing brings tangible production losses. It downgrades or rejects finished fasteners and raises rework cost. Direct metal‑to‑die friction speeds up die consumption, increases die‑changing frequency, lifts overall production cost and delays delivery schedule.Close technical coordination between steel wire supplier and fastener manufacturer is essential to suppress scuffing, realize stable high‑speed cold heading, extend die service life and raise overall production yield.