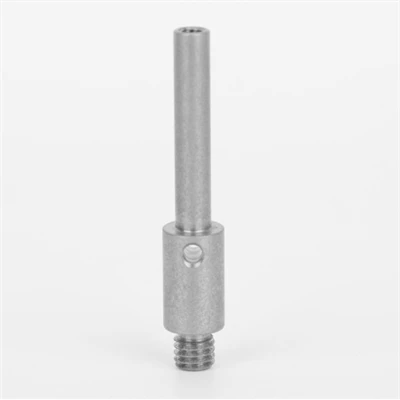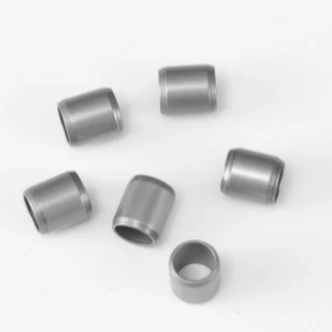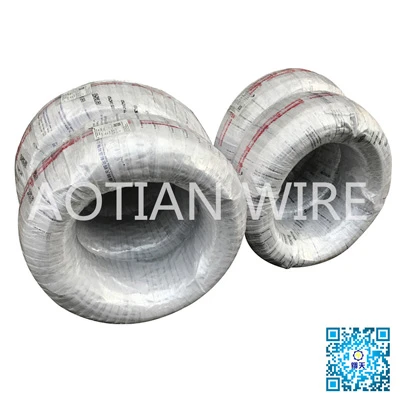

Cold heading steel is also called riveting steel or cold top forging steel, forming steel, cold heading is used at room temperature with one or more impact loading, widely used in the production of screws, pins, nuts and other standard parts. Cold heading process can save raw materials, cost reduction, and improve work by cold work hardening of the tensile strength, improve performance, cold heading steel must have good cold upsetting performance, reduce impurities such as S and P content in steel, strict quality of steel surface, often USES the high quality carbon steel, if steel containing carbon steel is more than 0.25%, should carry on the spheroidizing annealing heat treatment, To improve the cold heading property of steel.
Usually, the surface of cold heading steel wire produces a certain depth of small scratches called drawing. The cold heading steel wire after drawing is easy to crack after bolt forming and heat treatment, so the surface quality of the wire must be strictly controlled in the drawing process.
The flaring problem is caused by the sliding friction caused by the cold heading steel wire rod material sliding along the die surface. Therefore, the flaring problem usually occurs in the position of heavy material walking in the forming. The problem of drawing will aggravate the wear rate of drawing die, resulting in the instability of a large number of finished wires.
The factors affecting hair pulling include raw material factors and mould factors:
1.Raw material factor
The diameter of cold heading steel wire rod has been expanded from 5mm to 40mm to 4.5mm to 60mm. The diameter of round steel ranges from 20mm to 100mm. Steel material, diameter range, low carbon or medium carbon, etc. The larger the yield and tensile strength and diameter range of the material, the greater the forming force and sliding friction of the cold heading steel are required. Therefore, the more likely the cold heading steel wire is to have the tension problem. The larger the diameter range of cold heading steel is, the smaller the drawing Angle is, and the easier it is to have the drawing problem. When the tensile strength is greater than 650MPa, the diameter of the raw materials in the range of 24mm or more, the drawing speed is too fast, the problem is particularly prominent.
2.Mould factors
Mould factors mainly include mould material, mould hardness, mould clearance and surface finish. The die material with good toughness (wear resistance) and quenching performance (hardness value between 59-63HRc) can reduce the damage to the die caused by pulling hair. Most enterprises use hard alloy die, also useful alloy steel inserts Cr12MoV and SKD11. For materials with tensile strength of 440MPa, the method of reducing die clearance is often used to obtain a better clean surface size, but the problem of drawing will also be aggravated with the reduction of die clearance. The surface of the cold heading steel is not cleaned up, or the dirt on the die is not cleaned up. The surface of the die will form bond chips during the repeated drawing process, and these bond chips greatly aggravate the drawing defects.
The problem of drawing the finished wire can be solved from the Angle of pulling mould factor
Selection of hard alloy die, or with Cr12MoV and SKD11 alloy steel inserts, to ensure the hardness after quenching.
Regular maintenance of pull and pull die to ensure the surface smoothness of the working part of the inner hole.
Coating is made on the surface of the inner hole working part, such as TD treatment and PVD treatment, to improve the hardness and wear resistance of the inner hole working part.
In a word, for the common problem of finished silk wool drawing, we should do a good job of experience accumulation and summary, constantly optimize the production process and improve the process, to ensure the surface quality of finished silk.