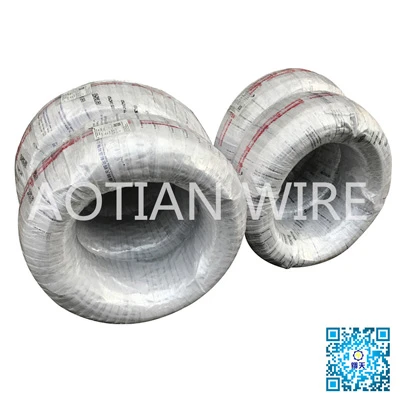

The screw wire needs to be processed before it can be put into screw production. The following is a brief introduction to the pickling and wire drawing process of the screw wire.
The purpose of pickling is to remove the oxide film on the surface of the wire and form a phosphate film on the metal surface to reduce the scratches on the mold during the wire drawing and cold heading forming process.
Pickling process:
1. Pickling: The entire disk element is respectively intruded into three hydrochloric acid tanks with a concentration of 20-25% at room temperature for several minutes, the purpose is to remove the oxide film on the surface of the wire.
2. Clearwater: remove the hydrochloric acid corrosion products on the surface of the wire.
3. Oxalic acid: increase the activity of the metal to make the film generated in the next process denser.
4. Coating treatment: The disk element is intruded into the phosphate, the steel surface is contacted with the chemical treatment solution, and the steel is dissolved to form insoluble compounds, which adhere to the steel surface to form a coating.
5. Clearwater: remove the residue on the surface of the film.
6. Lubricant: Since the friction coefficient of the phosphate film is not very low, it cannot give sufficient lubricity during processing, but it reacts with metal soap to form a hard metal soap layer, which can increase its lubricating performance.
The purpose of drawing the wire: too cold draw the panel element to the required wire diameter. Practically, for some products, it can be divided into two stages: rough pumping and fine pumping.
The workflow of the wire drawing:
1. Small wire drawing: Since the minimum size of the general disk element is 5.5mm, the wire diameter required for most small screws is relatively small, and the deformation of small screws is large when forming. In order to reduce the processing stress caused by cold drawing, and ensure For the machinability of the wire rod, the cold drawing of the wire rod is divided into two stages. First, the coil element is roughly drawn to a certain wire diameter by a continuous wire drawing machine and then annealed to eliminate the processing stress caused by rough drawing.
2. Large wire drawing: After the plate element is pickled, it is cold drawn to the required wire diameter by the wire drawing machine. It is suitable for wires used for large screws, nuts, and tooth bars.